


Pallet Conveyors and Transfer Shuttles
Automated equipment for conveying, orienting and distributing pallets and other heavy loads throughout warehouse and production flows.
Pallet Conveyors and Transfer Shuttles
Automated equipment for conveying, orienting and distributing pallets and other heavy loads throughout warehouse and production flows.
Automating pallet transport
Alstef Group designs and integrates conveying systems tailored to load characteristics, required throughput and the layout of each warehouse or production facility. Conveyors, transfer equipment, lifts and shuttles can be combined to move loads between production, storage, order picking and shipping areas.
These systems can be integrated into complete warehouse automation solutions and controlled to ensure continuous, traceable material flows.

Conveying systems for every application
Depending on travel distances, changes in direction or level, the number of transfer points and required performance, different technologies can be combined within the same system.
Conveyors
Convey, accumulate, orient and transfer loads between different areas of the facility.
Shuttles
Provide fast transfers between multiple points along a circuit and handle high-throughput flows.
Additional equipment
Inspect, identify and prepare pallets throughout their journey in the warehouse.
Conveying systems throughout the warehouse
Pallet conveyors
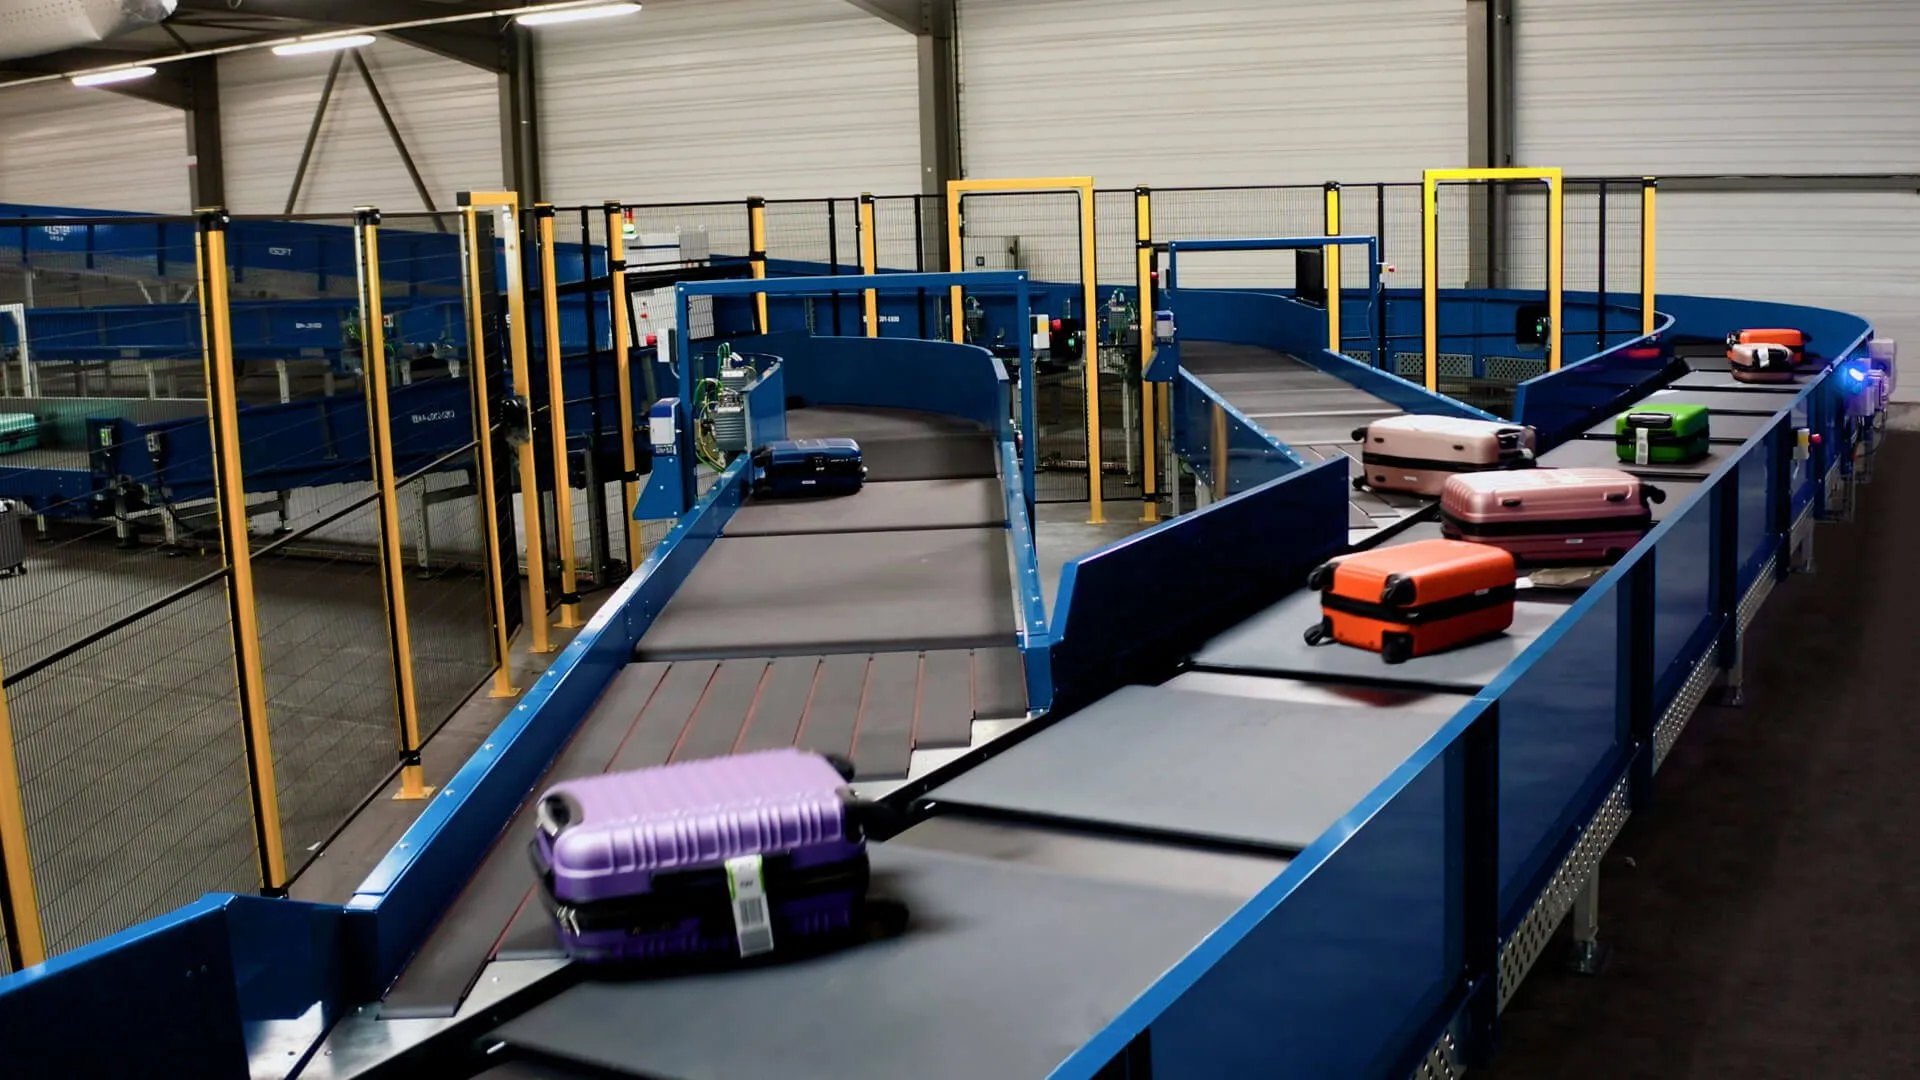
Conveyor systems provide continuous transport of pallets and other unit loads between the different stages of a warehouse or production process. Robust and reliable, they can handle high volumes consistently and are particularly suited to repetitive flows in warehouses and production facilities.
Their configuration is defined according to the load carrier, weight and dimensions, as well as required throughput, routes and interfaces with other automated equipment.
Roller and chain pallet conveyors
Roller conveyors transport and accumulate pallets along straight routes. They can be integrated at different points within the system, including storage infeed and outfeed, connections with production lines, order picking areas and shipping areas.
Chain conveyors transport pallets and heavy loads where the load carrier or its orientation requires a different handling method from a roller conveyor.

Transfers and changes in direction
Transfer modules change the route of a load and connect different sections of the conveyor system.
Transfer units can move loads from a roller conveyor to a chain conveyor, or vice versa.
Turntables can change the orientation of the load and/or its direction of travel.

Gravity pallet conveyors
Gravity conveyors enable pallets to be moved or accumulated without motorizing each conveyor section.
They are particularly suited to shipping areas, where they can create pallet queues awaiting loading and facilitate pallet staging at the dock.

Pallet lifts
When material flows need to move between different levels, lifts provide vertical load transfer and connect directly with the conveyor system. They can bridge height differences, serve different floors within a facility and help optimize the use of available space.

High-throughput pallet transfer shuttles
For pallet transport over long distances, or where flows require high throughput and fast transfers, shuttles provide an alternative or complement to continuous conveyor systems.
The vehicles are guided by a central rail installed either overhead or at floor level, depending on infrastructure constraints and associated costs. The rail supplies the energy required to power the shuttles.
Depending on the application, performance requirements, number and distribution of pick-up and drop-off points, and building configuration, Alstef Group selects the most suitable solution from its range.
The system can also evolve as requirements change, with additional shuttles added to increase capacity and accommodate changing material flows.

Additional equipment for pallet handling
Pallet conveying involves more than simply moving pallets. Additional equipment can be integrated directly into the conveyor system to inspect load carriers, identify pallets and prepare loads for subsequent stages of the process.
Load protection
Strapping, stretch wrapping and hooding equipment can be integrated into the conveyor system to secure palletized loads before storage, transfer or shipping.

Load identification and traceability
Labeling, barcode reading and RFID systems can be used to identify pallets and track them throughout the different stages of the process.

Pallet and load carrier quality control
Inspection equipment checks pallet conformity before entry into the automated system and identifies load carriers that could disrupt its operation.

Our pallet conveying and material handling projects




Complete warehouse automation solutions
Conveyor systems can be integrated into broader automation solutions combining automated storage, mobile robotics, order picking and control software, depending on the requirements of each facility.
Alstef Group designs and integrates these technologies to automate pallet and material flows from receiving through to shipping.